
Selecting a contract electronics manufacturer starts with matching the design and production requirements to documented capability. For SMT lines and complex assemblies, evaluate comparable project evidence, process controls, inspection coverage, and the supplier’s response to your files.
This guide provides a checklist for evaluating technical capability, assembly standards, inspection and test, DFM feedback, quotation scope, lead time, and communication. Use the questions to request evidence specific to your design rather than treating a generic capability claim as proof.
Apply the checklist to the requirements and evidence for your own project.
Ready to Start Your PCBA Project?
Send your assembly files, quantity, sourcing needs, and test requirements to discuss project scope and a confirmed quotation.
Request a Quote1. Manufacturer Experience and Technical Expertise
Look for documented experience with PCB technologies such as multilayer or rigid‑flex, and with component types comparable to your design. Request evidence of the relevant production and inspection processes.
Ask these questions early:
- How long has the factory produced comparable assemblies, and what evidence can it share?
- Can they share examples of boards with the same layer count, copper weight, and surface finish you use?
- Do they have in‑house engineering staff who give DFM feedback before the first run?
A manufacturer that only does simple consumer boards may struggle with a 12‑layer high‑density design for an aerospace application. Pcba manufacturer selection criteria start with this match: your complexity and their proven capability must align. No amount of marketing claims can replace a factory visit or a detailed audit of their process records.
2. Quality Standards: Beyond the Certifications
Ask for current ISO 9001 certification where required, and agree the applicable IPC‑A‑610 revision and assembly acceptance class. A management-system certificate and a product acceptance standard serve different purposes; verify how the supplier applies them to the proposed build.
Class 2 vs Class 3 – Choosing the Right Acceptance Level
IPC-A-610 provides acceptance criteria for electronic assemblies using specified product classes. Agree the class, standard revision, customer requirements, and any application-specific additions before quoting. Product class is a requirements decision, not a guarantee of a particular field-failure rate.
- Class 2 acceptance is commonly associated with dedicated-service electronic products. Evaluate the actual joint type and applicable standard revision; a single BGA voiding percentage does not describe every case or replace the agreed customer requirements.
- Class 3 has stricter acceptance criteria for specified assembly features. Agree the applicable standard revision, product class, inspection coverage, and any package-specific requirements before quoting; inspection time and cost depend on the design and test plan.
Choose the acceptance class from the product’s functional, environmental, reliability, and customer requirements. Medical and aerospace assemblies may have additional or different requirements; their application label alone does not establish one universal class. Ask the supplier to explain the resulting process, inspection, and quotation scope without assuming a fixed cost premium.
Where required, verify the applicable J‑STD‑001 soldering-process requirements and the supplier’s measurement controls. Ask whether solder-paste inspection is used after printing, what it measures, how exceptions are handled, and how its effectiveness is recorded; do not assume a universal defect-capture percentage.
3. Inspection and Testing Capabilities
AOI, X-ray, electrical test, and functional test cover different failure modes. Establish the defects relevant to the design and request a documented coverage plan rather than treating equipment names as complete proof of inspection capability.
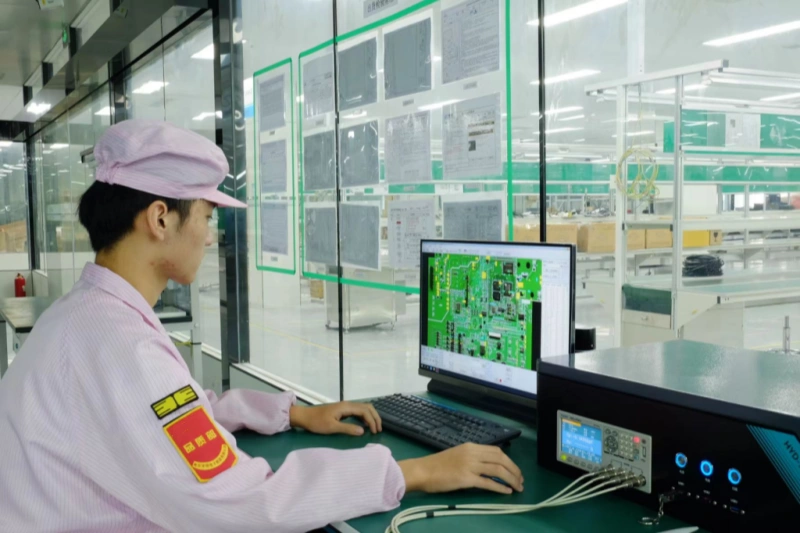
Beyond AOI: The Test Strategies That Save Field Returns
Consider complementary inspection and test stages, and request evidence of coverage and process performance for comparable assemblies:
- Inline AOI – Review coverage for visible features such as component presence, polarity, alignment, and selected solder-joint conditions. Agree sampling, programming validation, false-call handling, and any features that the camera cannot inspect.
- X-ray or CT – Review the method’s ability and limitations for the package and defect of interest. BGA wetting defects such as head-in-pillow can be difficult to establish conclusively from an image; determine whether complementary electrical tests, process evidence, or destructive analysis is needed.
- Flying probe electrical test – Depending on board access and the test program, this can check selected nets, shorts, opens, component values, or device behavior. Confirm actual coverage; it does not automatically test every component or eliminate the need for other methods.
For higher volumes, an in-circuit test fixture may be appropriate, depending on access, coverage, programming, and fixture cost. ICT does not necessarily test every net and component, nor test them all simultaneously. Match electrical and imaging methods to the design’s risks and document the untested features.
Define functional tests from the product’s operating requirements where needed. Inspection and electrical testing are complementary, and no single method proves every real-world condition. Evaluate effectiveness using documented coverage and results rather than a universal percentage reduction in field returns.
4. Technology and Equipment
Look past the generic “state‑of‑the‑art machinery” claims. Specific equipment determines what type of designs a factory can reliably run. A good evaluation covers these points:
- Placement speed and accuracy: Ask for validated package sizes, pitch limits, placement capability, and relevant first-article evidence. Confirm capability for the proposed BOM and board construction rather than inferring it from a machine brand or nominal placement speed.
- Soldering capabilities: Review the reflow profile, any nitrogen requirement, and the proposed selective, wave, or manual processes for through-hole parts. Ask the supplier to confirm the equipment and qualified process for the actual assembly.
- Rework and repair: Boards will fail, even in the best process. Ask if they have hot air rework stations and follow IPC‑7711/7721 for rework procedures. A factory without good rework capability will scrap boards that could be saved.
Request current factory and equipment evidence, together with the process limits relevant to the proposed assembly. A named equipment brand alone does not establish the supplier’s ability to meet your requirements.
5. Design Support and DFM Feedback
A factory‑level DFM (Design for Manufacturability) review is one of the strongest differentiators between a simple assembler and a true manufacturing partner. A good supplier will look at your Gerber files and BOM before quoting, not after you pay for a prototype run that fails.
Five DFM Topics to Check Before Assembly
Use the following DFM topics to structure the design review and request clear, design-specific feedback:
- Copper distribution and board support – Review copper balance, board thickness, panel design, and reflow support where warpage is a concern. Any added copper features must follow the designer’s electrical and mechanical constraints; empty copper areas alone do not prove that a board will warp.
- Solder‑mask‑defined (SMD) vs non‑solder‑mask‑defined (NSMD) pad mistakes – For fine-pitch BGAs, coordinate NSMD pad dimensions and solder-mask clearance with the package guidance and fabricator’s registration capability. Inadequate clearance can affect joint formation; confirm any pad or mask change with the designer.
- Panelization – Review support, tab locations, breakaway design, routing, scoring, and depaneling stress for the actual outline. Neither V-scoring nor routed tabs is universally suitable; agree panel changes and any engineering charges before release.
- Test-point access – Coordinate pad size, spacing, probe approach, clearances, and fixture requirements with the test provider. A 0.1-inch grid is not a universal ICT requirement, and fixture cost cannot be inferred from grid spacing alone.
- Silkscreen over pads – Check clearances between legend and solderable features against the fabricator’s rules. Agree any clipping or artwork changes with the designer before production.
Early DFM feedback can identify issues before fabrication or assembly, but the effect on prototype iterations and schedule depends on the design and the findings. Ask for a sample report and agree which changes require approval.
6. Prototyping and New Product Introduction (NPI)
Prototype turnaround depends on approved files, complete and suitable components, tooling, engineering review, test preparation, and available capacity. Ask the supplier to confirm the start conditions, minimum quantity, engineering charges, and completion date for the specific build.
What to Expect from a Quick‑Turn Prototype Run
For a quick-turn prototype, confirm the scope and completion conditions for these preparation steps:
- Gerber and assembly-file review: confirm the required approvals and the response time for unresolved questions.
- Component kitting: confirm who supplies each part, the approved sources, required quantities and attrition allowance, availability, and the date the complete kit is expected.
- Stencil and tooling preparation: confirm the release conditions, manufacturing time, and any special requirements.
Ask for a written project schedule that separates file approval, procurement, tooling, assembly, inspection, test, and dispatch. A quick-turn commitment should state the applicable quantity, design conditions, parts readiness, and available capacity; no fixed turnaround is assumed here.
For low-volume assembly, ask for the minimum quantity and a clear breakdown of stencil, programming, tooling, and test charges. Confirm whether any fee waiver or special term applies to the quotation rather than assuming prototypes are free of those costs.
7. Production Capacity and Lead Time
Capacity is not just about how many SMT lines a factory has; it is about how they schedule work to meet your deadlines. A small factory with good planning can deliver faster than a large one with overloaded schedules.
The Anatomy of a PCBA Lead Time
Request a project-specific lead-time breakdown with dependencies and milestones for each stage:
- DFM review and file approval – Confirm required inputs, review responsibilities, open questions, and whether purchasing can proceed before approval.
- Component procurement – Confirm stock status, approved sources, substitutions, logistics, and expected arrival dates for all parts.
- Production scheduling – Confirm line availability and the conditions for reserving capacity.
- Assembly – Confirm quantities, setup requirements, processes, and the planned build duration.
- Inspection and test – Confirm coverage, fixtures and programs, acceptance criteria, and time for resolving failures.
- Shipping – Confirm dispatch terms, transit estimates, customs responsibilities, and whether transit is included in the quoted lead time.
Distinguish the quoted assembly duration from the full time to dispatch or delivery. The total depends on approvals, procurement, tooling, capacity, inspection, test, and any rework; request a confirmed schedule for the specific order.
For higher-volume orders, ask what capacity is reserved for the project, how throughput is demonstrated, and how shifts or additional lines would be qualified. Do not infer weekly output from the number of machines alone.
Ready to Start Your PCBA Project?
Send your assembly files, quantity, sourcing needs, and test requirements to discuss project scope and a confirmed quotation.
Request a Quote8. Cost Factors and Pricing Models
Price matters, but the cheapest quote often hides risks: cheap component sourcing, no test, poor quality. A proper pcba quotation evaluation looks at the total cost, not just the per‑board assembly price. Pcba cost factors include:
- BOM cost – Review the approved supply chain, availability, alternates, traceability, and any customer approval required for non-franchised sources. Ask the supplier to document the sourcing plan for the actual order.
- Labor cost – Driven by the number of SMT placements, through‑hole parts, and any manual operations like conformal coating or potting. The assembly cost is often quoted per joint or per board.
- NRE (Non-Recurring Engineering) – Request separate charges for stencil, programming, fixtures, test development, and special tooling. State what can be reused on repeat orders and calculate the per-board allocation using the quoted quantity.
- Test development – Identify fixture, programming, validation, maintenance, and recurring test costs separately, with the agreed coverage and acceptance criteria.
Turnkey vs Consignment: A Total Cost Analysis
The choice between pcba turnkey vs consignment affects your cash flow and risk.
- Turnkey – The manufacturer buys the agreed components and may charge sourcing or handling fees under the quotation. You receive one invoice and a fully built board. This saves you inventory management, but you pay the fee. For an illustrative $50 BOM on 500 units, the base component cost is $25,000. A 10% procurement fee adds $2,500, giving $27,500 before assembly, tooling, tax, and shipping.
- Consignment – You supply the agreed parts; confirm any receiving, handling, storage, and assembly charges in the quotation. Agree an attrition allowance by package, quantity, packaging, and process; one percentage is not suitable for every kit. You also carry the risk of missing or counterfeit parts. On the same illustrative 500-unit order, the base component cost is $25,000 before attrition allowances, inventory costs, and any line-down costs from shortages. The net saving is often smaller than it appears.
Compare turnkey and consignment using the same approved BOM, quantities, sourcing assumptions, attrition allowance, fees, inventory costs, and responsibilities. Confirm which model the supplier offers and compare the complete quotation.
Confirm minimum order quantity, setup charges, and repeat-order terms with the supplier. Small builds can have a higher per-board cost when fixed engineering and tooling charges are allocated across fewer units; no universal minimum quantity or fee waiver is assumed.
9. Material Sourcing and Surface Finishes
PCB base materials and surface finishes directly affect assembly yield, reliability, and cost. A manufacturer should explain your options clearly.
- Base laminates: Confirm the exact grade, construction, thermal properties, and assembly qualification. High-Tg material can be appropriate for demanding builds, but Tg alone does not prevent delamination. Confirm availability and procurement time for the selected grade rather than assuming stock or a fixed delivery period.
- Copper weight: Review the required finished copper, feature geometry, current, temperature rise, and fabrication limits. Ask the supplier to confirm the proposed inner- and outer-layer construction instead of assuming a universal routine copper limit.
Surface finish is a common pcba surface finish comparison point because it affects solderability, shelflife, and flatness. Here is a quick reference:
- HASL (lead-free) – Evaluate surface planarity against the package and pitch requirements, along with solderability, storage, and assembly constraints.
- ENIG (Electroless Nickel Immersion Gold) – A planar finish commonly considered for fine-pitch packages. Confirm plating requirements, solderability, packaging, and the supplier’s specified storage conditions and shelf life.
- OSP (Organic Solderability Preservative) – A planar finish that requires appropriate handling and storage. Confirm the specific finish process, permitted assembly exposures, packaging, and shelf life.
- Immersion silver – Evaluate planarity and solderability together with handling, packaging, storage, and tarnish controls. Use the supplier’s finish-specific shelf-life requirements.
- Immersion tin – Review solderability, storage, permitted assembly exposures, and any tin-whisker requirements for the application.
Choose the finish using the package geometry, assembly profile, storage plan, reliability requirements, and documented supplier process controls. Where ENIG is used, discuss controls and inspection for nickel corrosion and related solder-joint risks rather than assuming the finish is risk-free.
10. Communication and Customer Support
Agree the project contact, update frequency, escalation route, and access to inspection and test records. Clarify which of the following services are included in the quotation:
- Order-status and inspection-data access, with an agreed format and update frequency
- A process for reporting availability changes and obtaining approval before component substitution
- First-article reports or remote build reviews where agreed
Assess response quality as well as response time. Agree business hours, time-zone coverage, urgent escalation, and expected reply times for technical or supply issues; a particular email response time does not establish production-crisis performance.
11. Supplier Audit: A Practical Checklist
You do not need to visit every factory, but a structured pcba supplier audit checklist can be used remotely or on‑site. Use these points:
- Quality management: Request the applicable current management-system certificates and verify their scope. For IPC-A-610, distinguish trained or certified personnel from a claim that a factory or product has blanket certification; request evidence of the agreed assembly acceptance process.
- Process Control: Ask for a sample PFMEA (Process Failure Mode and Effects Analysis) for a similar board. If they cannot produce one, process discipline is weak.
- Incoming Inspection: How do they verify components? Do they have a digital microscope and X‑ray for spot‑checking?
- Equipment Maintenance Records: Ask for the last calibration certificate for their SPI and AOI machines.
- Traceability: Ask which materials, lots, process steps, inspections, and tests can be traced to an assembly, and request a representative record. Confirm the marking and retention requirements for the project.
- Rework Documentation: Request their IPC‑7711/7721 rework procedure. Good rework prevents field failures.
- Environmental Compliance: Verify RoHS and REACH compliance. Ask for conflict minerals reporting if needed.
Use this checklist to score potential suppliers. A “no” on traceability or documented process control is a red flag.
Frequently Asked Questions
How do I choose a PCB assembly company?
Start with a clear list of your technical requirements: board layers, component types, expected volume, and required quality class. Then use this article’s pcba manufacturer selection criteria to shortlist factories, check their DFM feedback, and evaluate their testing and communication. Always ask for a sample build before a full production order.
What certifications should a PCBA manufacturer have?
Select required management-system certification, assembly standards, acceptance class, and application-specific approvals from the product and customer requirements. Ask for current certificates where relevant and evidence that the supplier can apply the agreed process and acceptance criteria to your build.
How much does PCBA cost per board?
Per-board cost depends on BOM, quantity, setup, process complexity, tooling, inspection, and test. Request an itemized quotation and separate recurring costs from one-time charges. Compare equivalent scopes rather than assuming a generic price range applies to the design.
What is the difference between turnkey and consignment PCBA?
In turnkey work, the supplier sources the agreed parts and builds the assembly under the quotation’s sourcing and handling terms. In consignment, the customer supplies agreed materials, while receiving, handling, attrition, storage, and shortage responsibilities still need to be defined. Compare total costs and responsibilities rather than assuming consignment has no handling charge.
How long does PCBA manufacturing take?
Lead time depends on file approval, material availability, tooling, production capacity, inspection, test, and shipping scope. Ask for a written schedule with start conditions and milestones for the specific build; distinguish assembly duration from the complete order cycle.
What is a DFM check and why is it important?
A DFM review checks the design against the proposed manufacturing and assembly processes, including pads, solder mask, clearances, panelization, and test access. Agree the review scope, deliverables, charges, and approval process before relying on it to resolve design risks.
Conclusion
Choosing the right PCBA manufacturer is not about finding the cheapest quote or the fanciest website. It is about identifying a partner that understands your technical needs, communicates transparently, and brings real manufacturing discipline. Use the pcba supplier audit checklist above, look for evidence of real DFM engagement, and demand specific test strategies, not just buzzwords.
Use the checklist to request documented capability, a design-specific DFM review, a test-coverage plan, and an itemized quotation. Confirm the applicable assembly standards, process limits, responsibilities, and schedule before placing the order.
Contact us today to get a design review or a fast, transparent quotation. We are happy to walk you through our process and show you exactly how we build quality into every board.